 EN
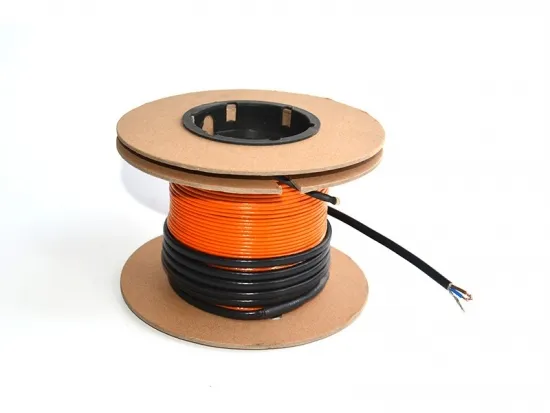
Many procurement teams and system designers focus heavily on upfront unit price when selecting heating cable, yet overlook long‑term reliability. Field‑based technical experience shows that poorly‑specified heating cable often suffers sheath cracking, power drift or premature breakdown within just a few operational seasons, generating high repair, replacement and downtime costs. Long‑term‑ready heating cable is defined not only by printed datasheet figures, but by material performance, verified compliance, consistent thermal output and solid manufacturing backing. Below we break down the core criteria for selecting durable heating cable for industrial, commercial and residential projects.
High‑Grade Material Construction for Extended Service Life
Material composition forms the physical foundation of long‑term heating cable performance. Premium‑grade heating cable applies multi‑layer structural design with carefully selected raw materials for conductors, insulation, outer jacket and metallic shielding layers. High‑purity conductive materials reduce resistance shift under repeated thermal cycling. Modified polymer or fluoropolymer jacketing delivers resistance against UV radiation, moisture, chemical vapors and mechanical abrasion, which are common failure triggers in outdoor, buried or plant‑site environments. A robust metallic braid shield provides continuous grounding and extra mechanical protection.
Industry standards such as UL 1674 and IEC 62395 specify material aging requirements for heating cable exposed to repeated cold‑hot cycles. Whether for process temperature maintenance, pipe freeze‑protection or snow‑melting tasks, durable heating cable requires raw materials formulated to resist thermal degradation over thousands of operating hours, rather than relying on low‑cost recycled polymer blends that degrade rapidly in harsh surroundings.
Rigorous Third‑Party Certification & Compliance Validation
Visible certification marks represent independent third‑party verification, rather than mere marketing logos. For global‑deployed heating cable, key credentials include CE, UL, CSA, ATEX and IECEx certifications, each covering strict test sequences including high‑voltage withstand, long‑term thermal ageing, flame retardancy and hazardous‑area safety assessment.
Certified heating cable has passed standardized accelerated ageing tests simulating years of real‑world operation. For end‑users and engineering contractors, valid certification delivers trustworthiness: it proves products satisfy regional safety codes for Europe, North America and other global markets. Without these verified qualifications, even attractively‑priced heating cable may fail site acceptance audits and create hidden safety risks for long‑run operation.
Stable Electrical‑Thermal Performance Under Continuous Operation
Excellent static parameters on specification sheets do not guarantee real‑world long‑term behaviour. Expert evaluation focuses on sustained electro‑thermal stability under continuous or cyclic working conditions. Quality heating cable maintains controlled power output with limited deviation after thousands of thermal cycles, avoiding serious power drift that causes insufficient heating or unexpected thermal stress.
Resistance to thermal stress is critical. Heating cable expands and contracts repeatedly as temperatures rise and fall. Well‑engineered products mitigate internal material fatigue to prevent insulation breakdown. Comprehensive factory‑level testing, including insulation resistance checks, power consistency sampling and environmental simulation, filters out latent defects before products leave production workshops. This transparent testing workflow reduces early‑stage field failures and supports multi‑year stable operation.
Full‑Chain Manufacturing & Application‑Oriented Technical Support
Durable heating cable solutions depend on more than individual component quality; they rely on complete industrial‑chain control from material formulation to finished‑product inspection. A capable manufacturer maintains in‑house laboratories for ongoing performance testing, together with patent‑backed process know‑how and flexible production capacity to match diverse project requirements.
Anhui Huanrui Heating Manufacturing Co., Ltd operates a large‑scale production facility with full‑range international certifications and more than 18 years of heating cable development experien. Its in‑house quality‑control system covers raw‑material screening, multi‑step production monitoring and finished‑product verification. The company also provides global‑oriented OEM and ODM services, supporting custom‑configured heating cable solutions for varied working environments.
When sourcing heating cable for long‑term deployment, buyers should balance initial cost with expected service life, certification status and manufacturer technical capability. Investing in well‑validated, quality‑built heating cable minimizes lifecycle expenditure and delivers stable heating performance year after year.